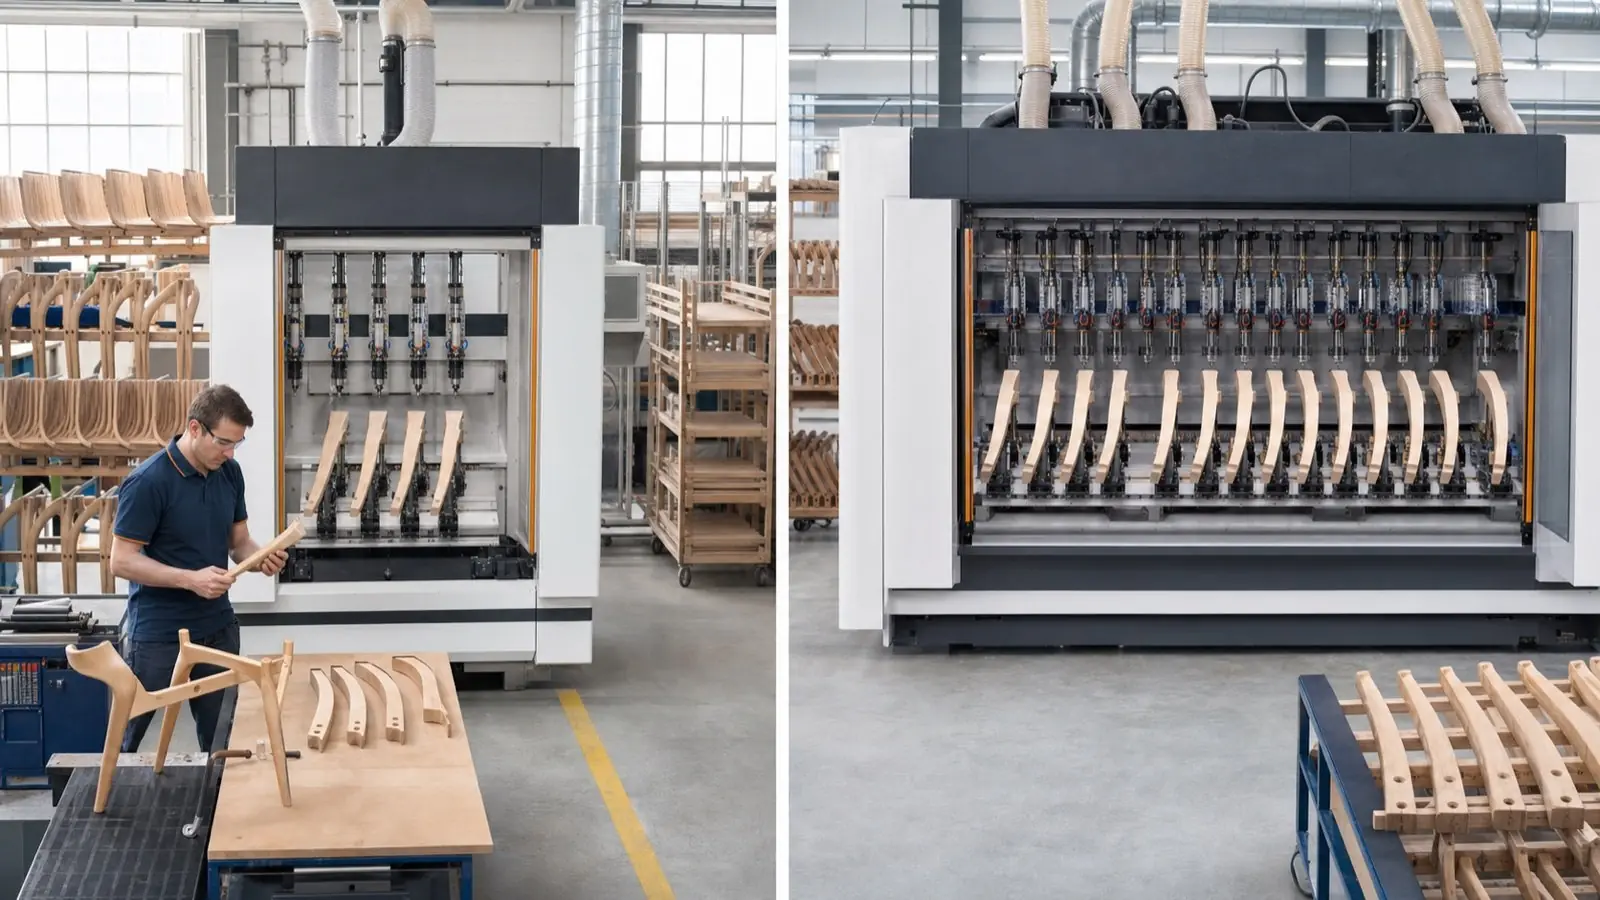
More machining heads can process more workpieces, but head count does not tell the whole story. A 16-head double-station machine and a 32-head single-station machine may suit very different factories. The right choice depends on part mix, batch size, loading method and how often you change programs.
Начните с производственной задачи
Multi-head machining centers are used for repeated drilling, milling and grooving on solid wood parts. Chair factories may use them for rails, legs, frames and other components that need the same operations in several positions.
The important question is not “Which machine has more heads?” It is “Which machine produces more good parts in my real shift?”
Что такое 16-шпиндельный двухстанционный станок?
The Jasper MD-1200D4 uses 16 machining heads and two work stations. Its standard example is four workpieces in one cycle. The two-station layout can help organize loading and machining, especially when batches change more often.
Что такое 32-шпиндельный одностанционный станок?
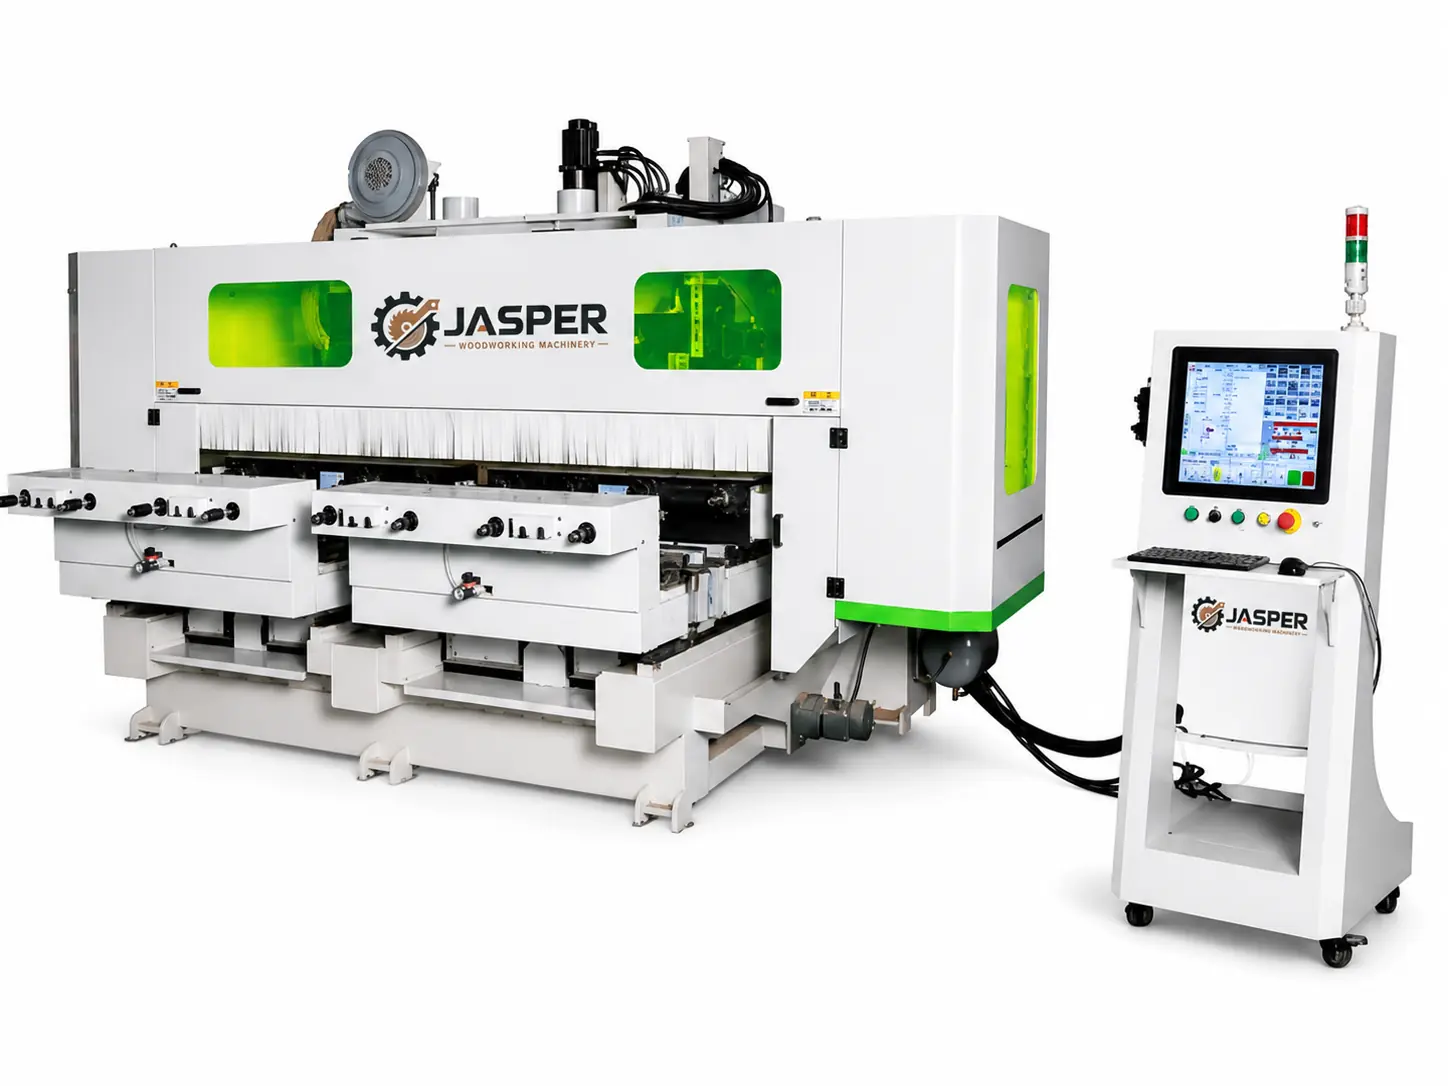
The Jasper MD-1200D8W uses 32 machining heads in one station. Its standard example is eight workpieces in one cycle. This layout is designed for larger repeated batches where the same setup can stay in production longer.
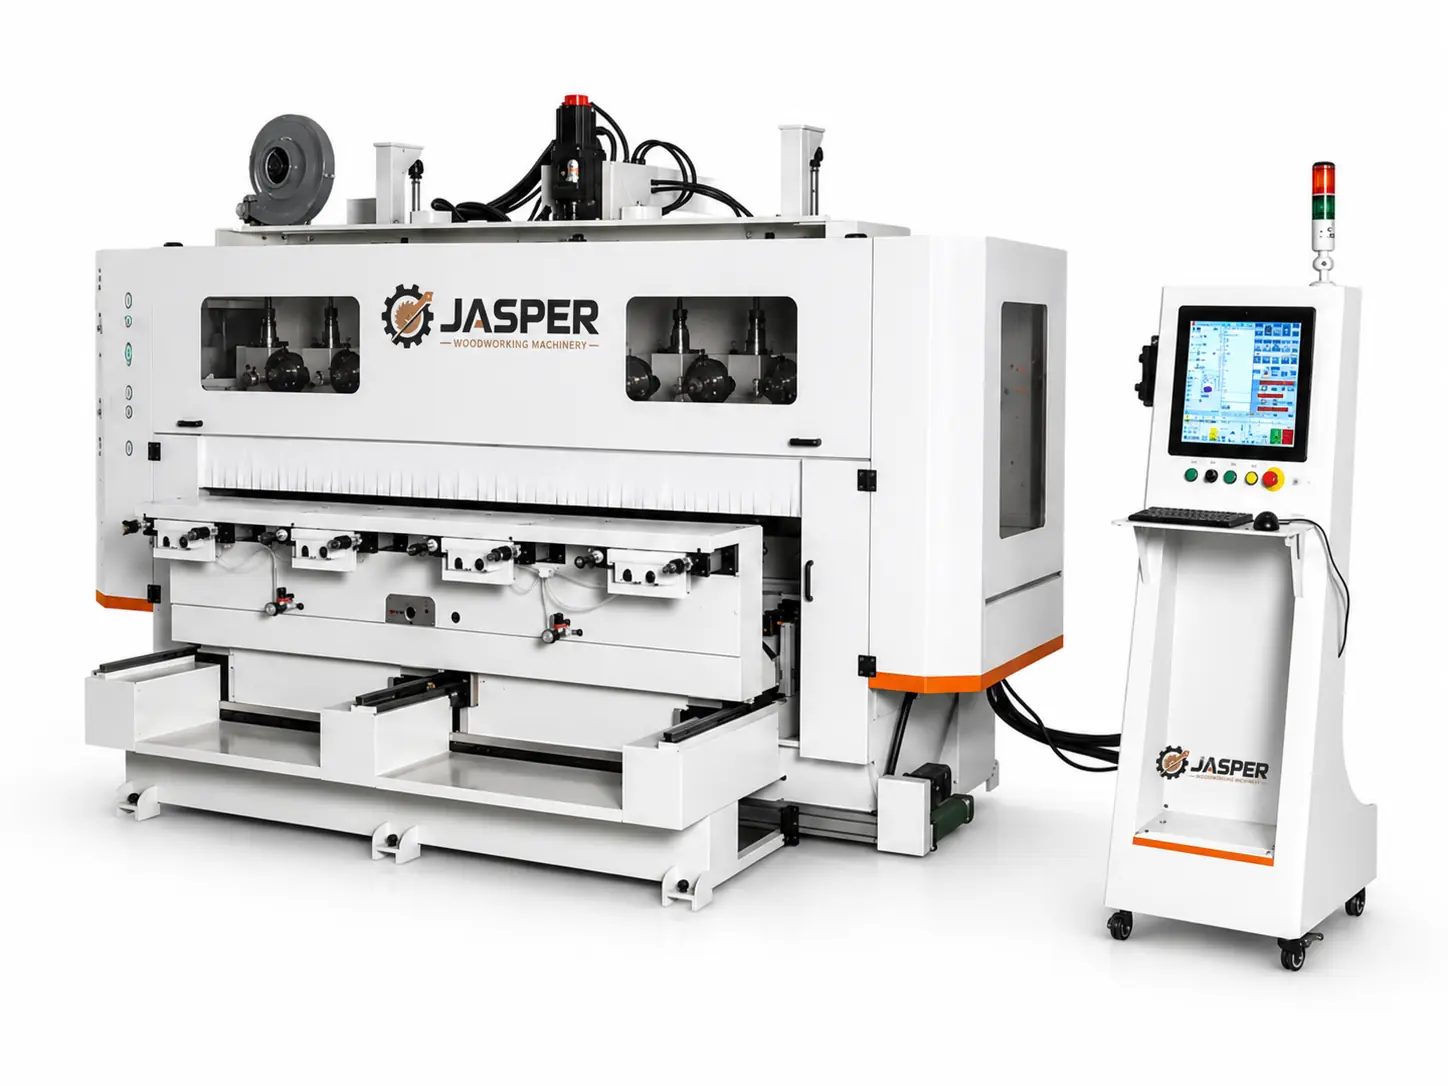
Важно: actual output depends on the part, fixture, toolpath, loading time and quality checks. The standard workpiece count is a configuration reference, not a guaranteed hourly result.
16- и 32-шпиндельный обрабатывающий центр
| Критерий выбора | 16 шпинделей, две станции | 32 шпинделя, одна станция |
|---|---|---|
| Пример стандартного цикла | 4 заготовки | 8 заготовок |
| Компоновка станций | Две станции | Одна станция |
| Оптимальное применение | Смешанные или часто меняющиеся партии | Стабильные повторяющиеся крупные партии |
| Особенности загрузки | Work can be organized across two stations | A larger group is prepared for one station |
| Ценность наладки | Useful when flexibility matters | Useful when one setup runs for longer |
| Основной риск | Too little capacity for growing volume | Unused capacity if batches are small |
Когда подходит 16-шпиндельная модель
- You produce several chair or furniture part types during one shift.
- Order sizes are small to medium.
- Programs and fixtures change regularly.
- You value a two-station workflow for loading and organization.
- You want capacity that matches present demand without leaving many positions empty.
Когда подходит 32-шпиндельная модель
- You run large batches of the same component.
- Eight matching workpieces can be prepared and loaded together.
- The same program and fixture remain in use for long production runs.
- Your upstream cutting and downstream handling can keep the machine supplied.
- Your current bottleneck is machining capacity, not material preparation or inspection.
Не сравнивайте производительность только по числу шпинделей
A larger machine can have more theoretical capacity, but empty fixture positions produce nothing. Slow loading, frequent program changes or unbalanced upstream work can also reduce the benefit.
A simple first estimate is:
Good parts per cycle ÷ cycle minutes × 60 = theoretical parts per hour
For example, four good parts in a five-minute cycle equals 48 theoretical parts per hour. Eight good parts in the same five-minute cycle equals 96. Real output will be lower after loading, setup, inspection, tool changes and normal downtime. Use your own measured cycle data, not these example numbers, for a purchase decision.
Пять вопросов для вашей производственной команды
- How many identical parts are in a normal order?
- How many part changes happen in one shift?
- Can every fixture position be filled in most cycles?
- How long do loading and unloading take?
- Can the previous and next processes support the planned output?
Почему важна пробная деталь
Send a real drawing and sample blank before confirming the machine. The supplier can review tool access, clamping points, head arrangement and the sequence of operations. A test also helps reveal whether the part can share one setup with other products.
For chair parts, small differences in curves, hole positions and grain direction can change the fixture. This is why a drawing-based review is more useful than choosing from a brochure photo.
Итог
The 16-head double-station machine supports a flexible four-workpiece workflow. The 32-head single-station machine supports a larger eight-workpiece workflow for repeated batches. Choose the model you can keep productively loaded. Consistent use of the right-sized machine is more valuable than unused maximum capacity.