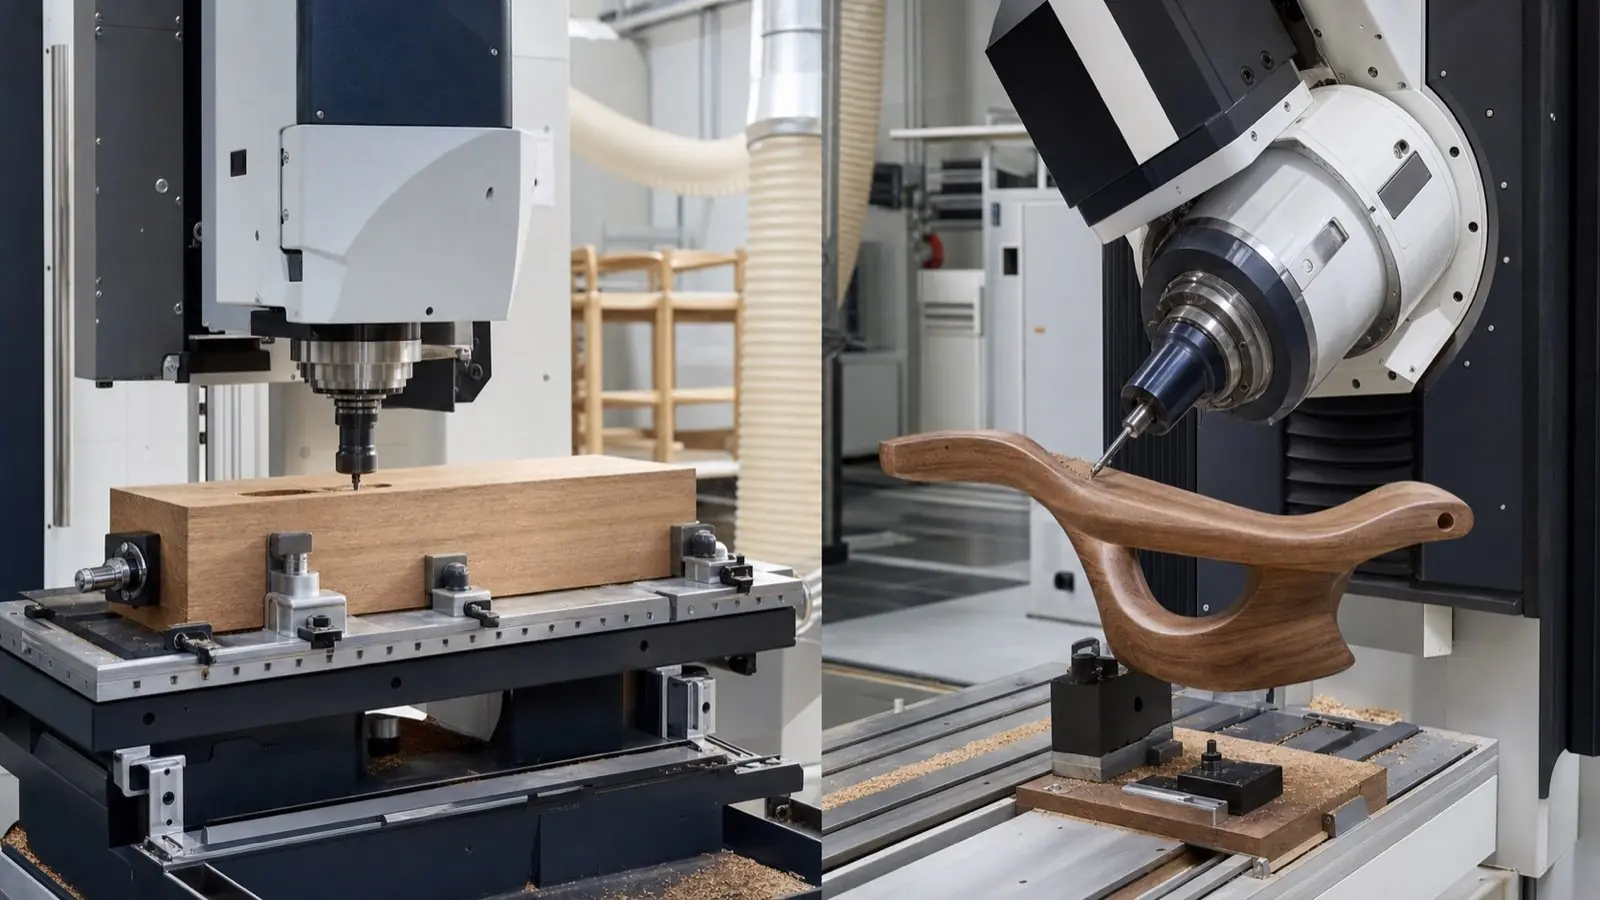
“Five-side” and “five-axis” sound almost the same. They are not. Five-side describes the faces a machine can reach. Five-axis describes how the machine moves. Understanding this difference can prevent you from buying more complexity than your parts need—or too little ability for curved work.
الإجابة السريعة
A مركز تشغيل خماسي الجوانب usually works on the top and four side faces of a part in one setup. It is a practical fit for drilling, grooving and milling on box-shaped or straight components.
A ماكينة CNC خماسية المحاور adds rotary movement to the tool or workpiece. This lets the cutting tool approach curves and angles from many directions. It is a better fit for complex chair parts, curved rails, angled joints and free-form surfaces.
خماسية الجوانب تصف الوصول. وخماسية المحاور تصف الحركة.
ما هو التشغيل خماسي الجوانب؟
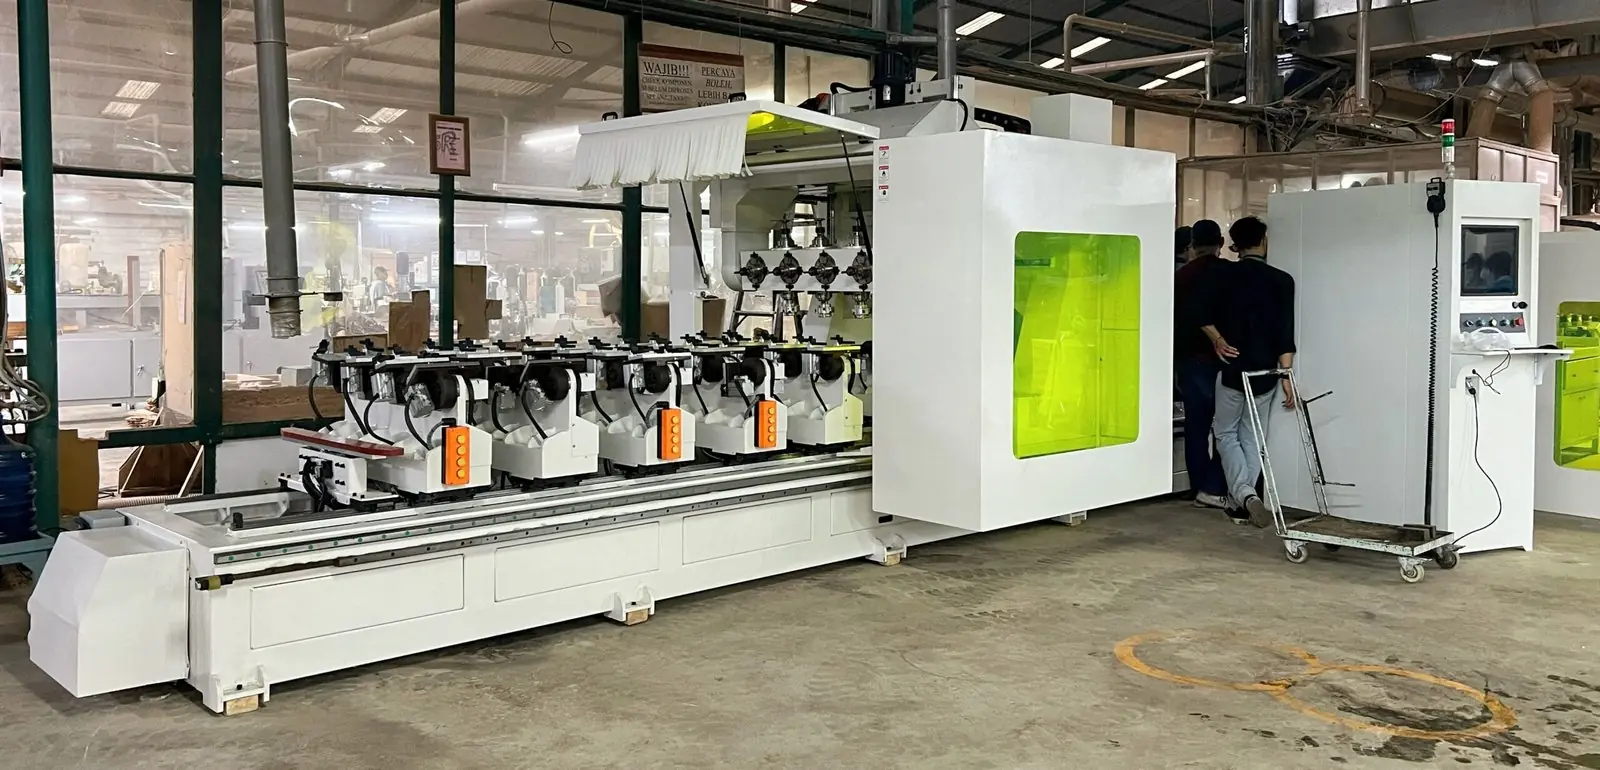
Imagine a rectangular furniture part fixed on a table. A five-side machine can process the top, front, back, left and right sides without turning the part by hand. The bottom stays against the fixture.
The machine may drill side holes, cut grooves, mill pockets and prepare joints. Because the part stays in one setup, the position between these features can be more consistent than a workflow with several manual clamping steps.
ما هو التشغيل خماسي المحاور؟
A basic three-axis machine moves along X, Y and Z. A five-axis machine adds two rotary axes. The spindle or the workpiece can tilt and rotate, so the tool can follow changing angles and curved surfaces.
This ability is important for parts such as chair armrests, curved back rails, complex legs and angled mortise-and-tenon joints. Some machines use all five axes at the same time. Others use the rotary axes to position the tool and then cut. Ask the supplier which motion the machine and software support.
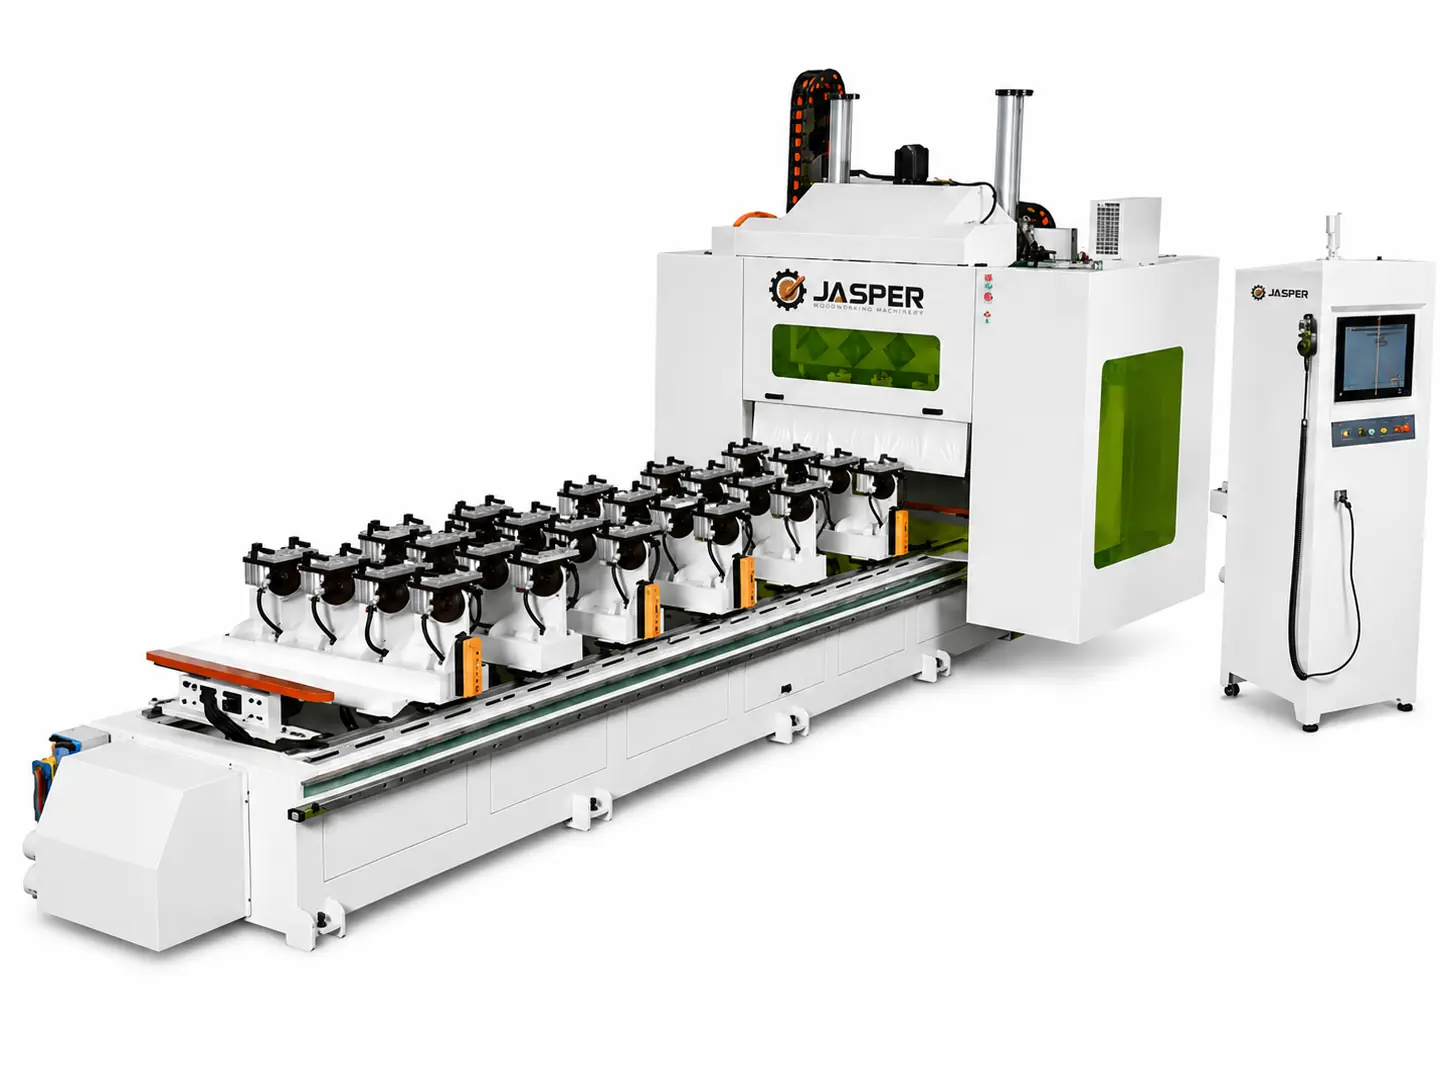
ماكينة نجارة CNC خماسية الجوانب مقابل خماسية المحاور
| نقطة القرار | CNC خماسية الجوانب | CNC خماسية المحاور |
|---|---|---|
| ما معنى الاسم | خمسة أوجه يمكن الوصول إليها | خمسة محاور حركة متحكم بها |
| أفضل شكل للقطعة | مستقيمة غالباً أو صندوقية الشكل | منحنية أو مائلة أو حرة الشكل |
| العمل النموذجي | Top and side holes, grooves and pockets | Surface machining, angled cuts and complex joints |
| البرمجة | عادة أكثر مباشرة | يتطلب عادة عملاً أكثر تقدماً في CAM |
| متطلبات التجهيز | Stable single setup for five faces | Must allow tool access around complex geometry |
| قيمة جيدة عندما | Reclamping is the main problem | Part geometry is the main problem |
اختر التشغيل خماسي الجوانب عندما...
- Your parts have mostly flat faces and straight edges.
- You need holes or grooves on several sides.
- Repeated manual turning creates errors or slow handling.
- Your programs use common drilling and milling operations.
- Your goal is to combine several simple operations in one setup.
اختر التشغيل خماسي المحاور عندما...
- Your parts include curves that change through space.
- The tool must enter the wood at changing angles.
- You machine chair arms, curved rails, sculpted legs or irregular components.
- You need angled mortise, tenon, end cutting or shaped surface work.
- A three-axis or five-side process would require too many fixtures and setups.
أربع تكاليف يغفل عنها المشترون غالباً
1. البرمجة time
A five-axis machine can make a complex part, but the toolpath still needs to be planned and checked. Include CAM software, post-processing and operator training in the decision.
2. Fixtures
The fixture must hold the part without blocking the tool. Curved wood can be harder to locate than a rectangular blank. A good fixture is part of the process, not an accessory.
3. Tool reach
Long tools can reach deep areas, but they may also vibrate more. The machine supplier should review the drawing, tool length and cutting direction together.
4. Real machine use
A five-axis machine only earns its place when its extra motion removes real setups or makes parts that simpler equipment cannot. If most of your work is drilling straight holes on five faces, a five-side machine may be easier to run and easier to keep busy.
اختبار قرار بسيط
Take your three most common parts and mark every machined feature on the drawings. Then ask:
- Can all features be reached from the top and four sides?
- Does any surface or joint need a changing tool angle?
- How many times is the part clamped in the current process?
- Which setup creates the most errors or delay?
- Can the operator and software team support five-axis programming?
If the main issue is access to five flat faces, start with five-side machining. If the main issue is changing geometry and cutting angle, study five-axis machining.
الخلاصة
Five-side machining is about reaching more faces with fewer setups. Five-axis machining is about controlling the cutting direction around complex shapes. Do not choose from the name alone. Choose from the features on your real parts, the fixtures they need and the skills required to run the process every day.