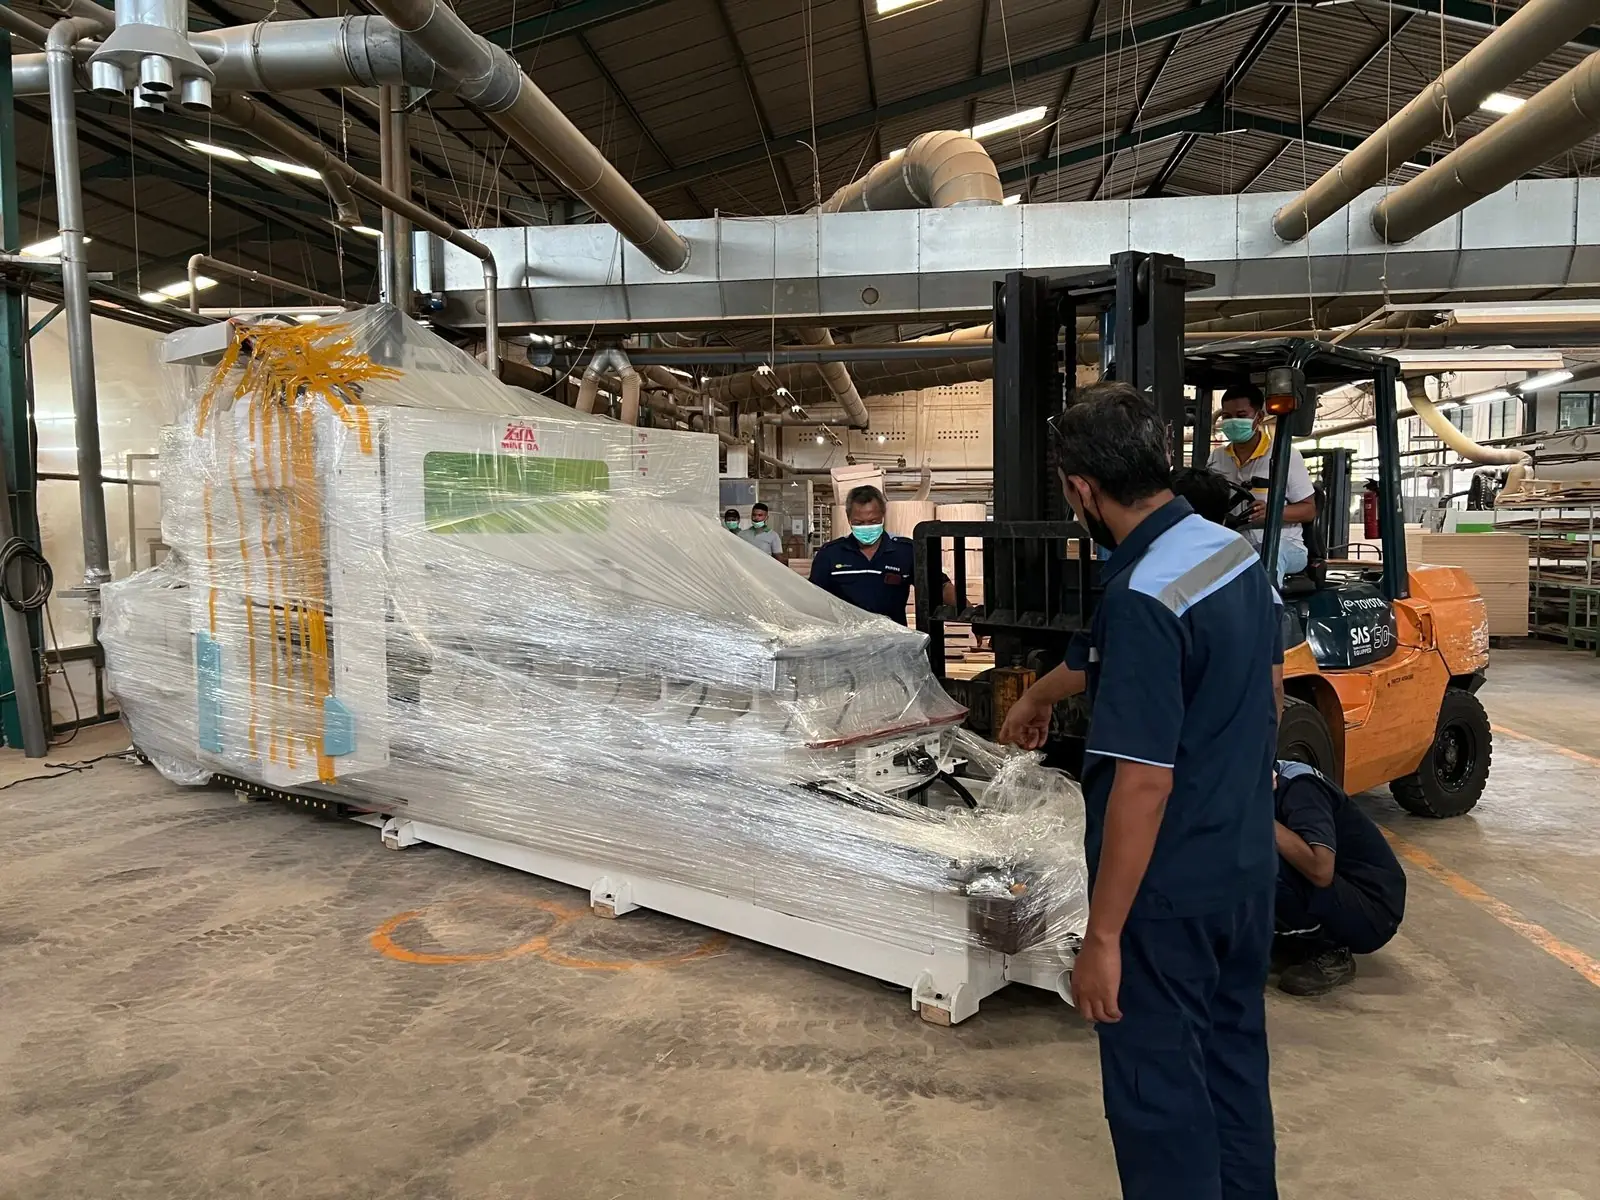
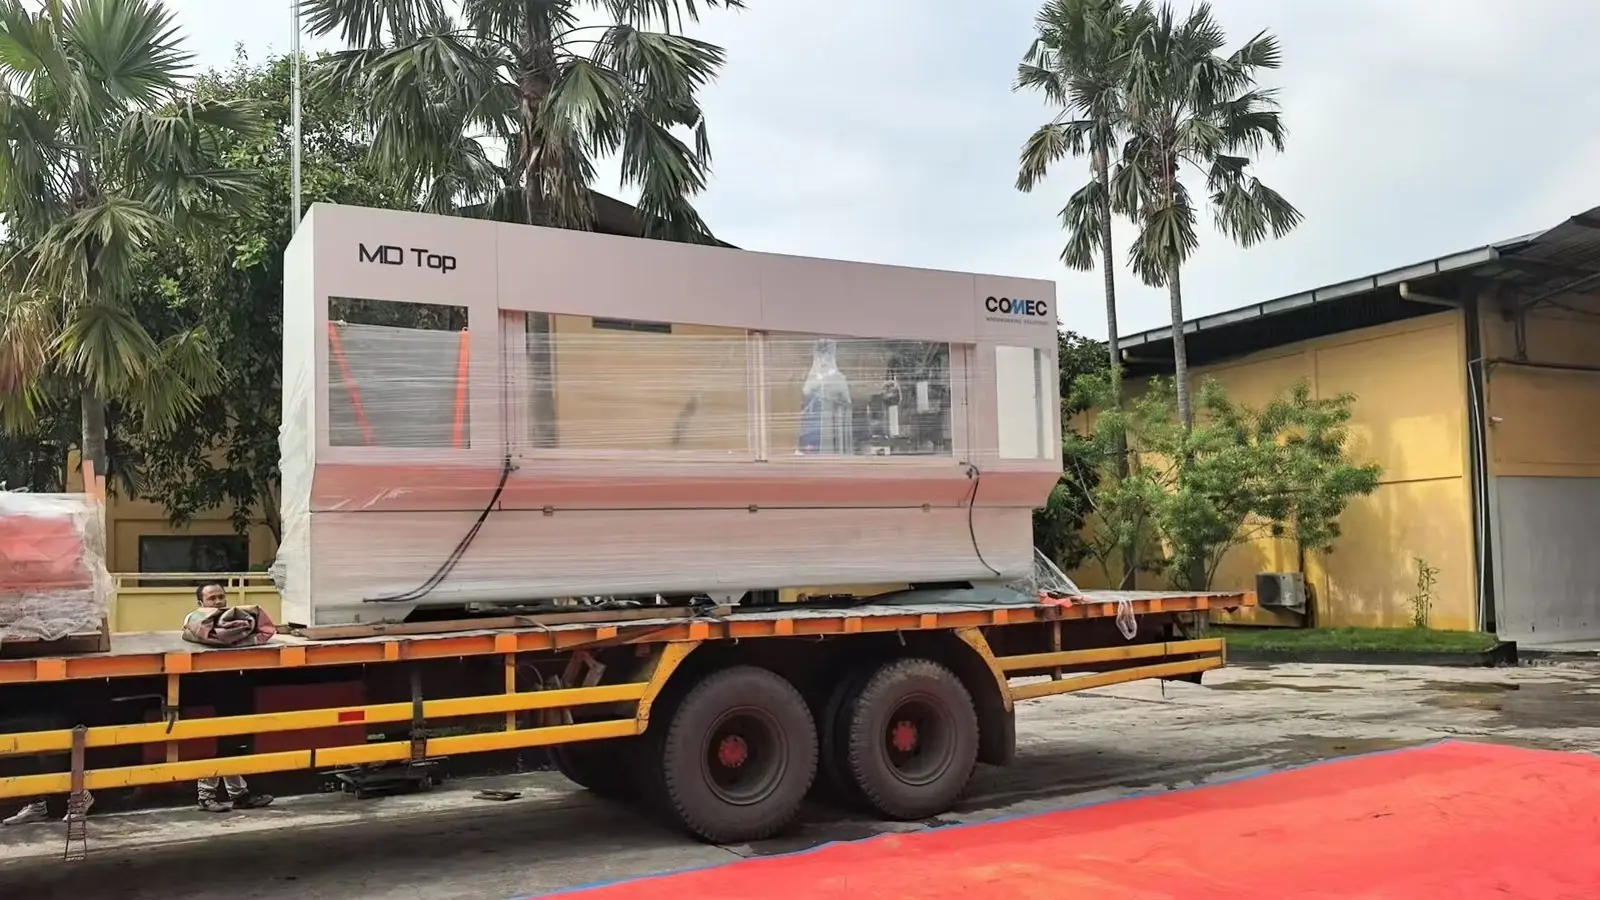
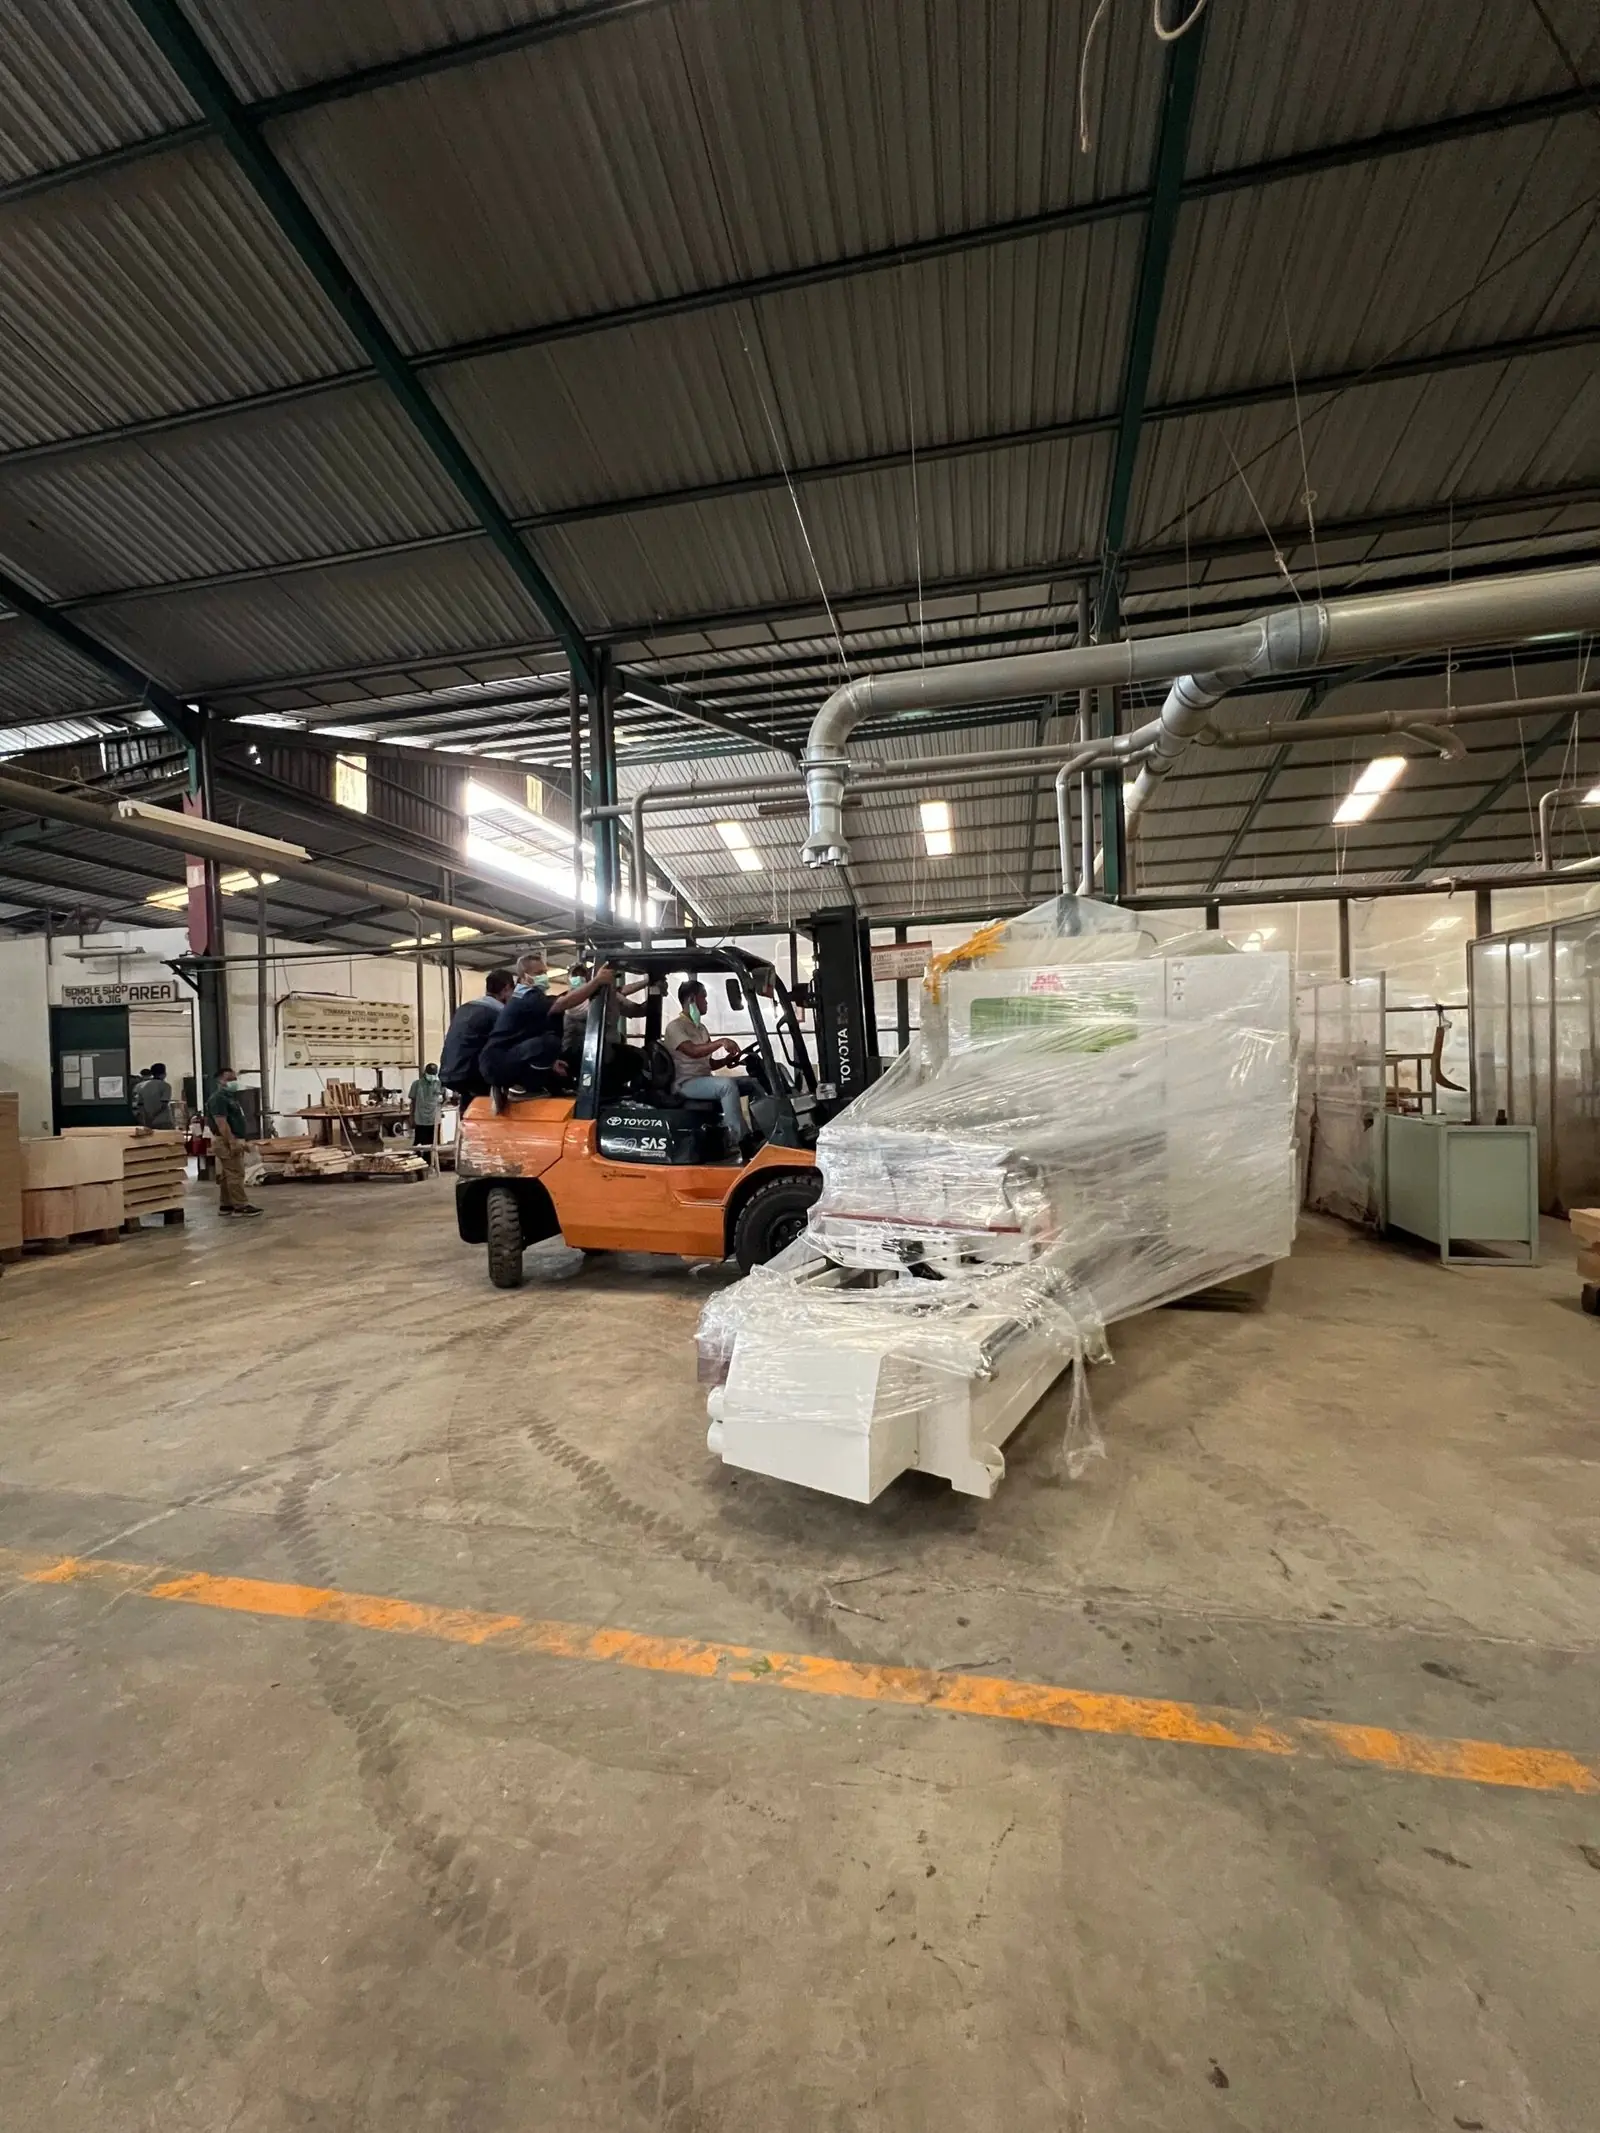
Machine installation at Danwood furniture factory in Indonesia
Indonesia · Documented Project Record

Danwood Indonesia: Chair-Component CNC Workflow

A documented implementation using a 16-head machining center and a five-side machining center for repeat chair and solid-wood furniture components. The public project record covers delivery, installation, operator training and technical support; it does not include a public time study or inspection log.

Client: DanwoodIndustry: High-End FurnitureApplication: Chair Components
2Documented Machining Systems
On-siteInstallation and Training Recorded
Chair partsPublished Application Scope
Project recordAcceptance and Test-Machining Noted
Customer Background

What the published project record identifies

The project materials describe Danwood as an Indonesian high-end furniture manufacturer serving international markets. The documented application is repeat chair and solid-wood furniture components.

The public materials do not provide a production baseline, machine inventory or independently verifiable output target. This page therefore treats the customer and production context as project-record information, rather than as a benchmark for other factories.

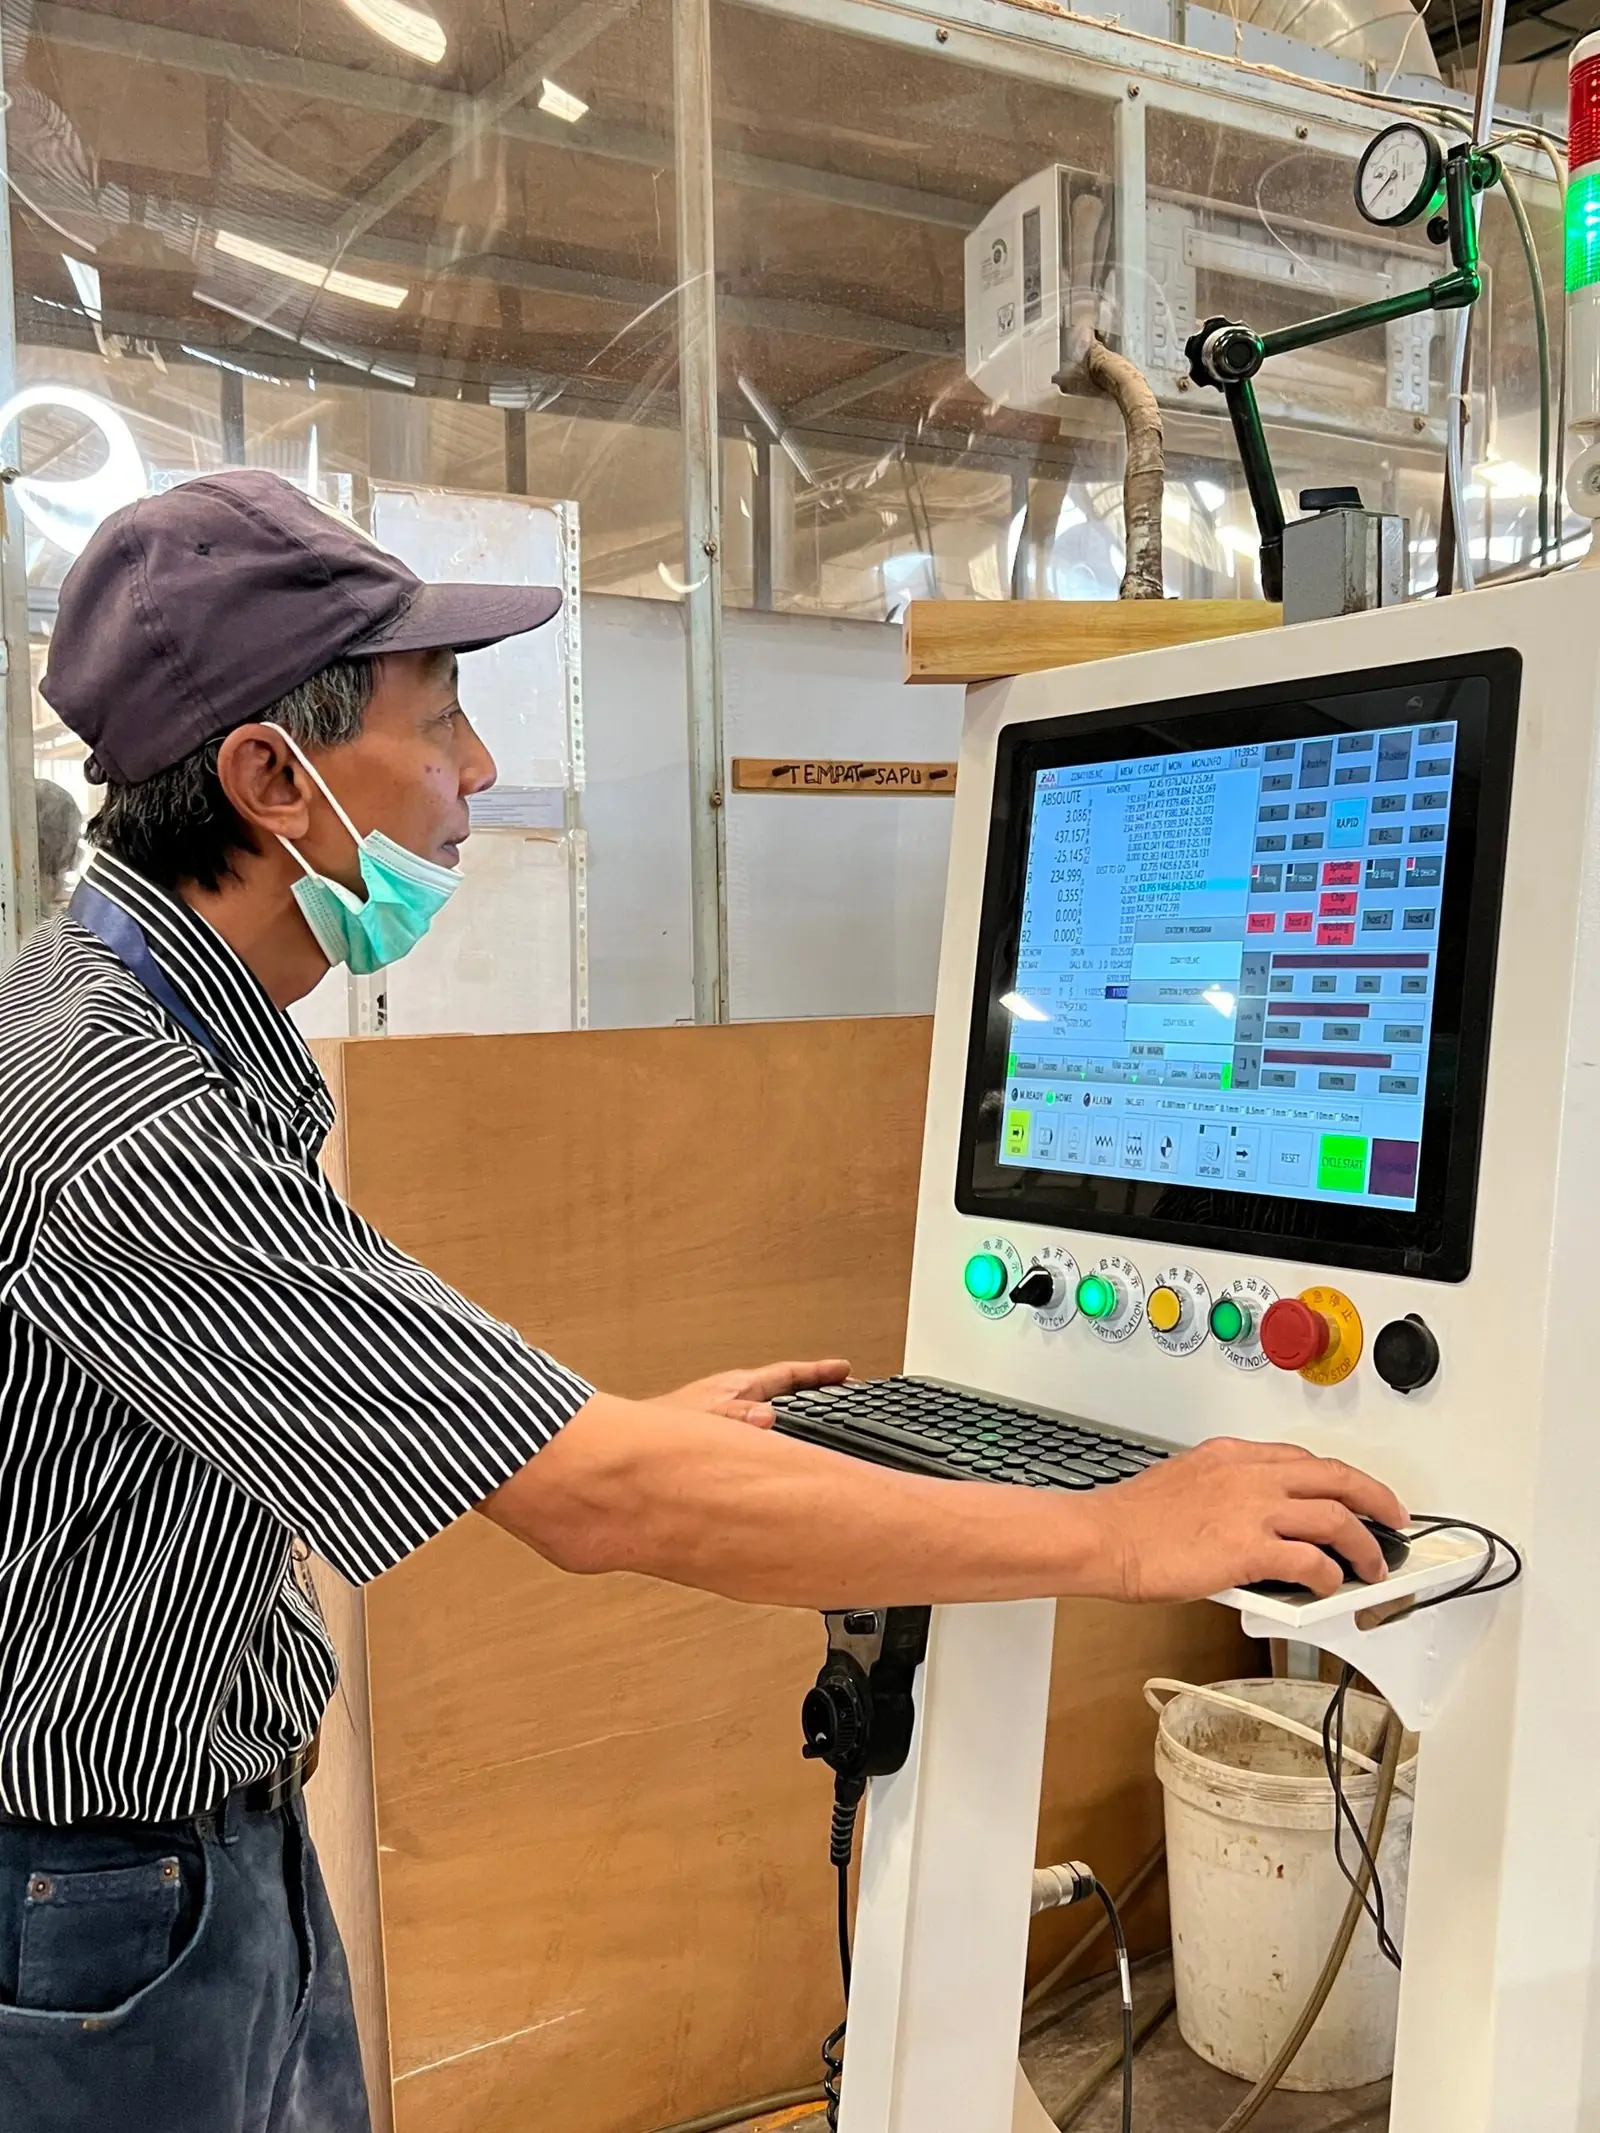
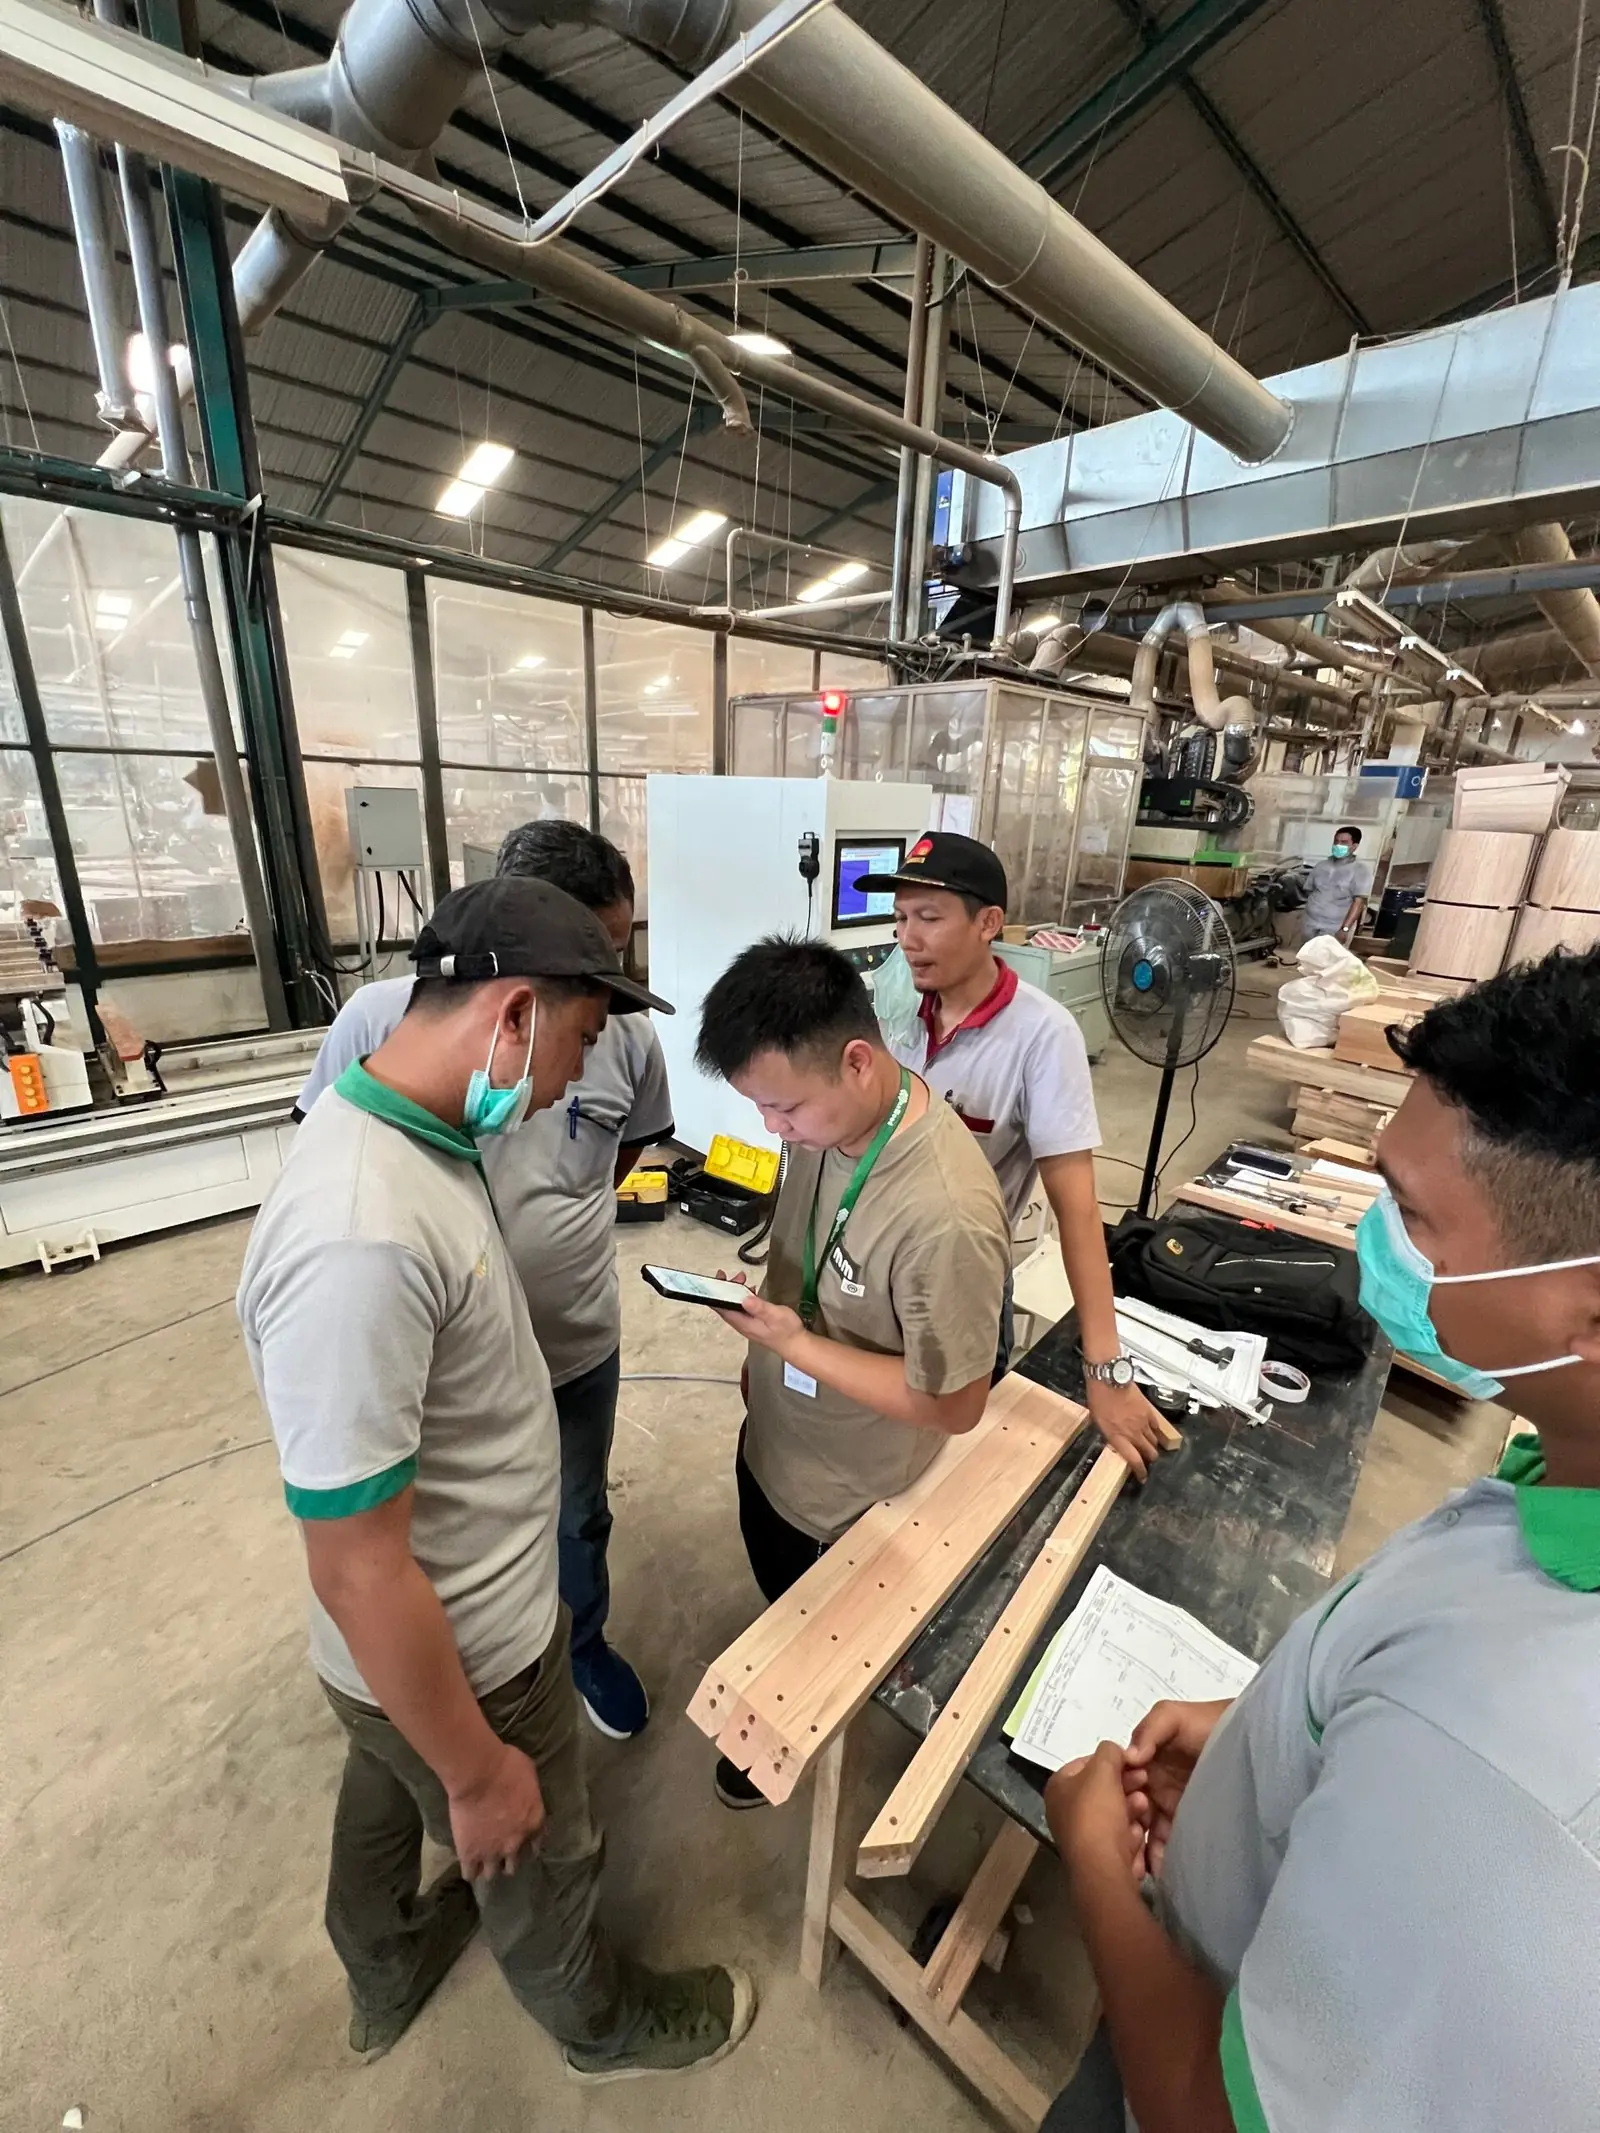
Danwood operator working with the CNC control system
Production Challenge

Recorded process objectives

The project materials identify the following workflow objectives. They are project requirements, not independently measured results.

01Process repeat chair and solid-wood furniture components.
02Combine drilling, milling and grooving within the planned workflow.
03Limit unnecessary reclamping and transfers where the part program allows.
04Support machining on multiple accessible faces.
05Establish an installation, training and technical-support handoff.
Project Configuration

Two documented machining systems

The published project record identifies these systems for the chair and solid-wood component workflow. Exact tooling, workholding, program strategy and part dimensions are not published.

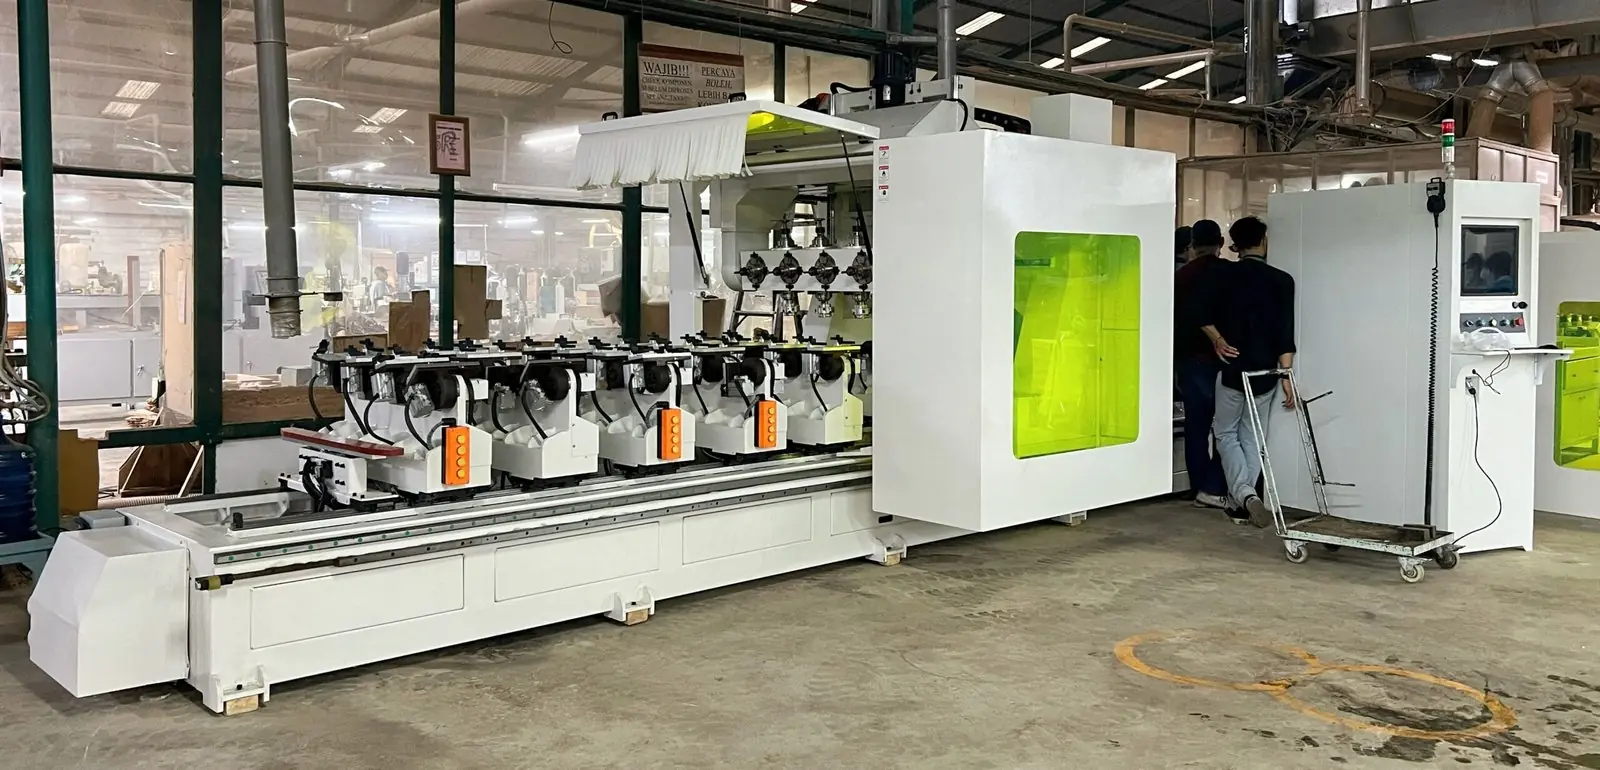
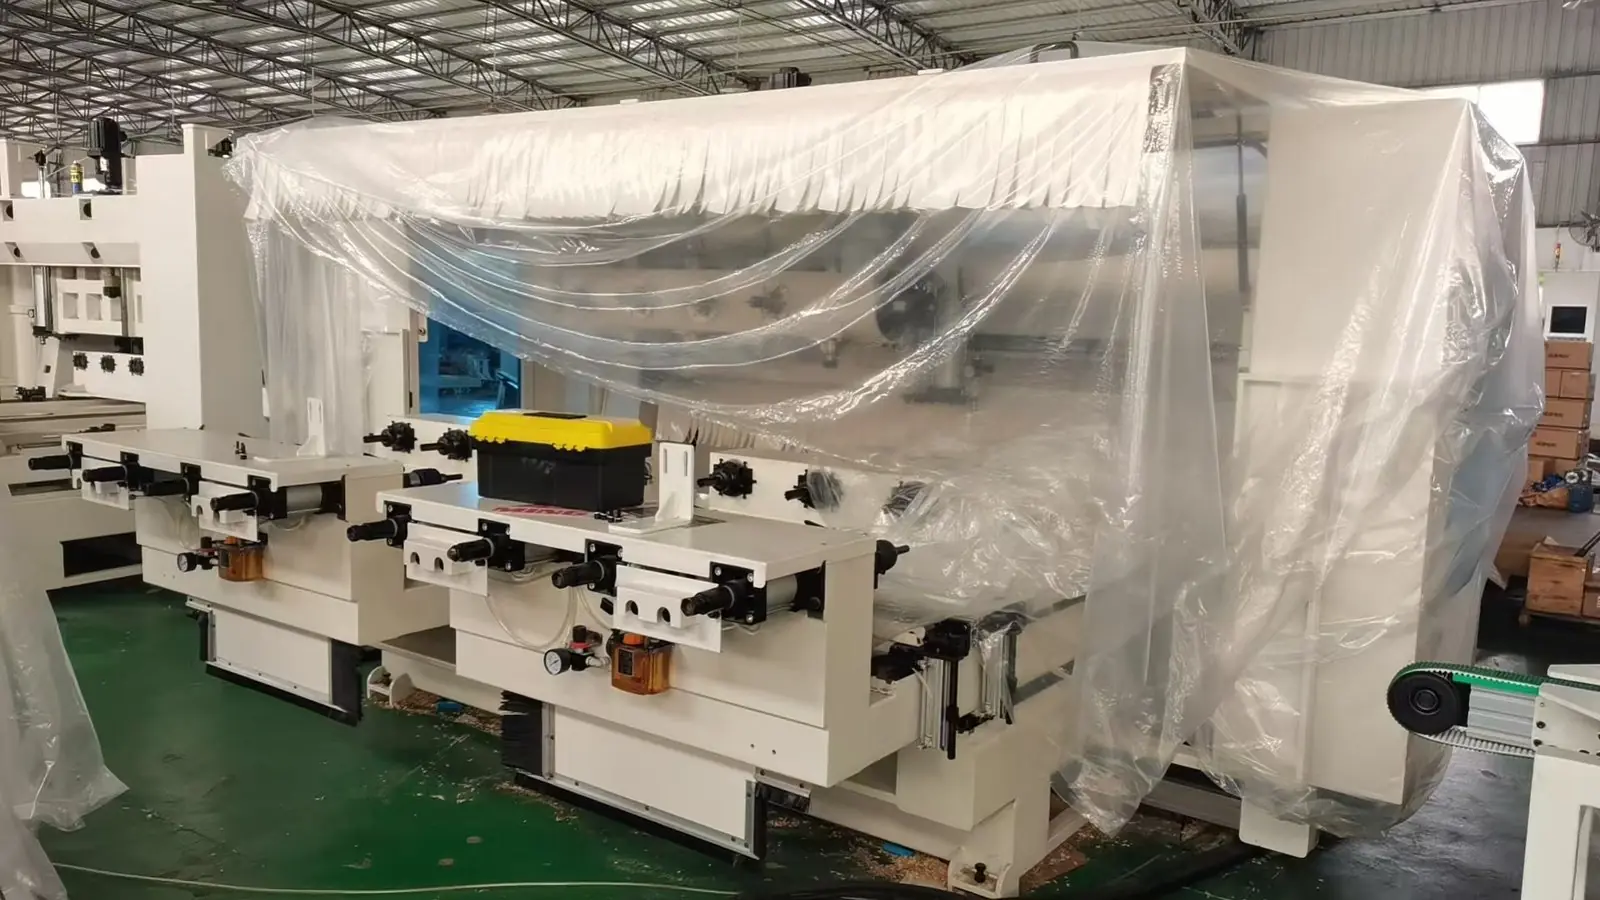
16-Head Machining Center documented for the Danwood project
System 01

16-Head Machining Center

The project record identifies a 16-head machining center for drilling, milling and grooving of chair parts, solid-wood components and repeat furniture parts. The record does not publish a cycle-time comparison or a verified tool-change count.

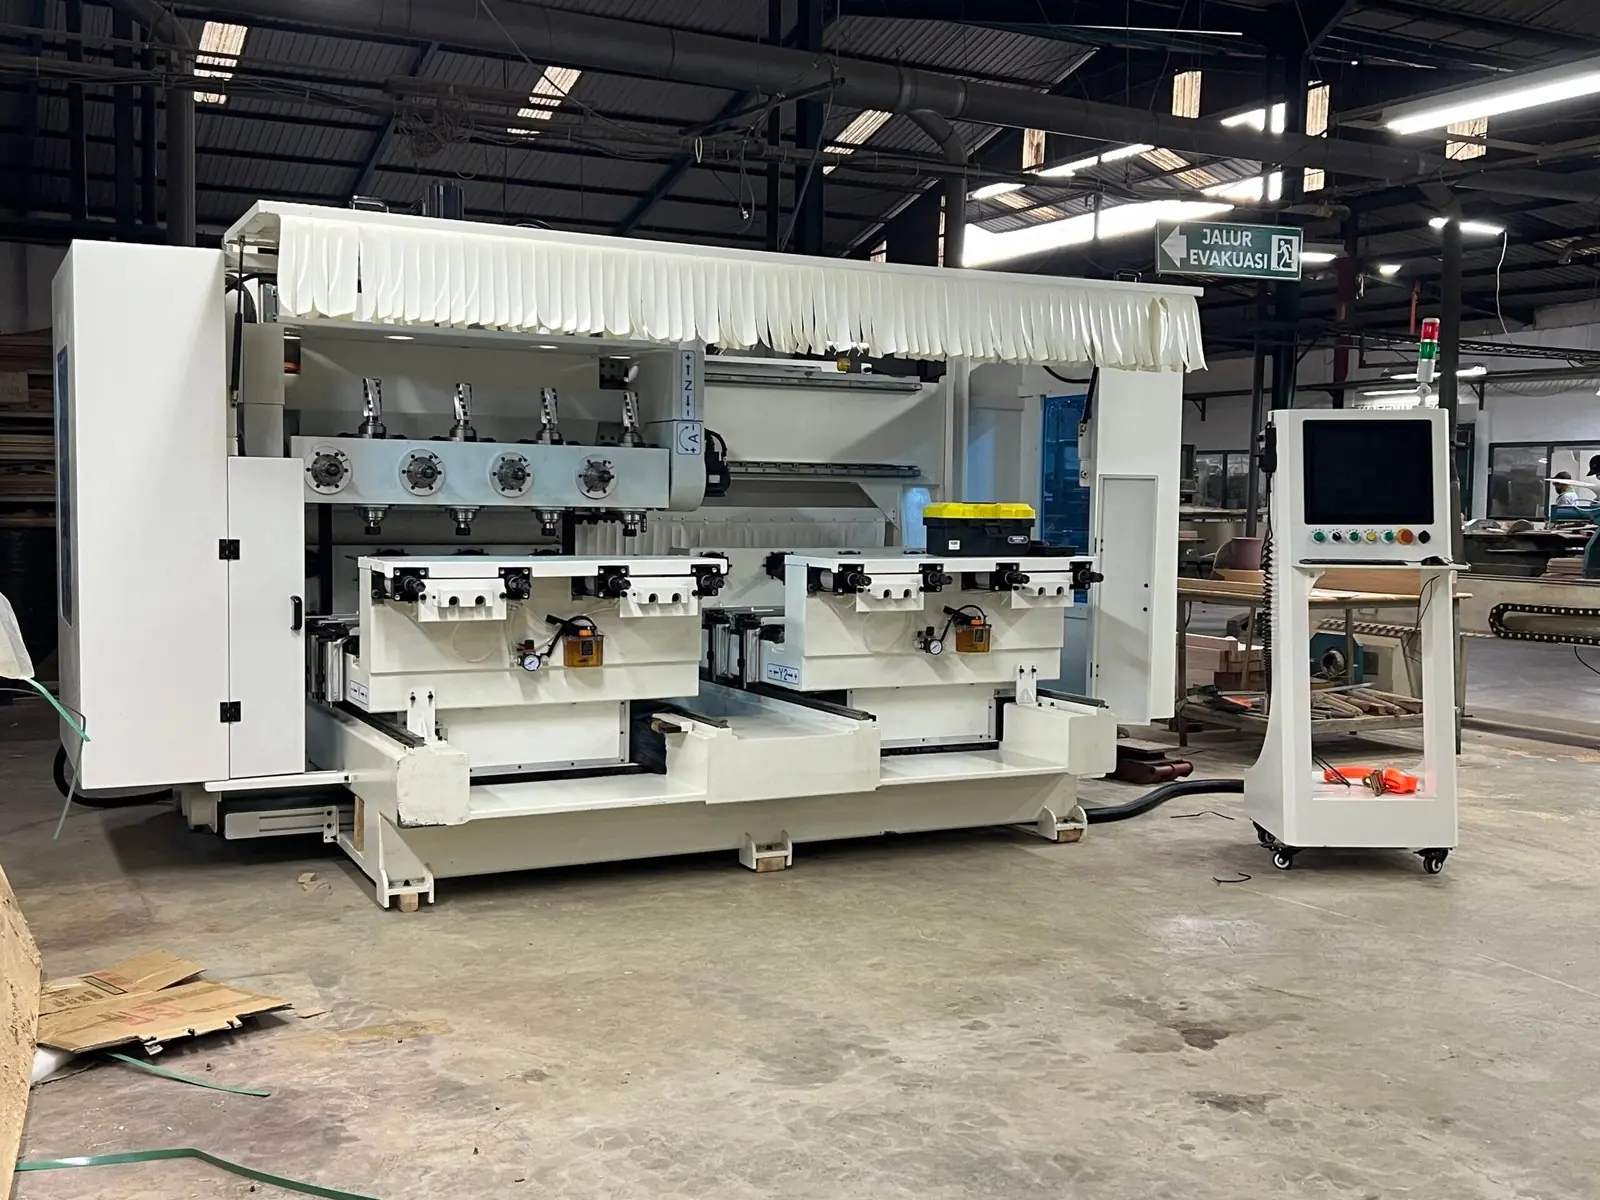
Five-Side Machining Center documented for the Danwood project
System 02

Five-Side Machining Center

The project record identifies a five-side machining center for multi-face drilling, milling, grooving and irregular processing. The public record does not state a universal accuracy tolerance or the exact number of setups used for each part.

On-Site Installation

Installation, training and production handoff

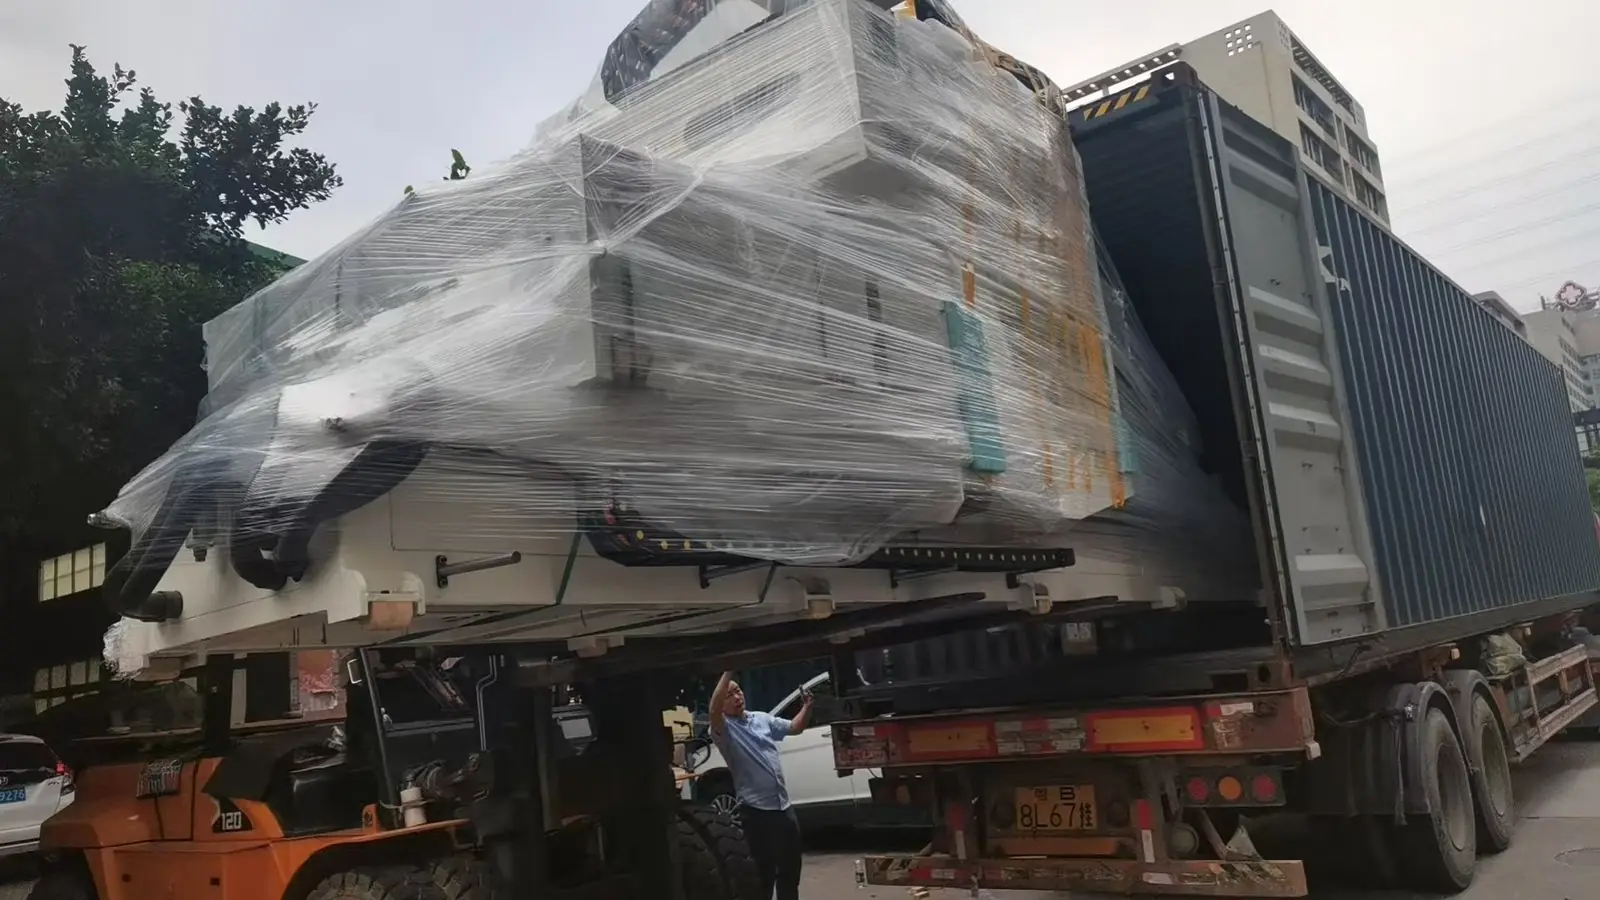
Project media and notes record delivery, installation, operator training and coordination with a local service team. Calibration tolerances, acceptance criteria and the final production start date are not published in the public record.

Project Gallery

From delivery to production readiness

After-Sales Support

Recorded support pathway after handoff

The project record notes an equipment-use and acceptance report, test machining, parameter discussion and operator training. It also records a WhatsApp support workflow between the customer, local dealer team and Jasper engineers. The underlying acceptance report and service-response data are not published here.

Jasper after-sales support for the Danwood project
Verification and Scope

What this case record verifies — and what it does not

This page reports a documented implementation. It does not use public headline figures for throughput, accuracy, scrap, capacity or delivery time because the supporting measurement method and inspection records are not available in the published project materials.

Documented: the project identifies a 16-head machining center and a five-side machining center for chair and solid-wood furniture components.
Documented: delivery, installation, operator training, test-machining and an ongoing technical-support workflow are described in the project materials.
Not publicly verified: baseline and post-installation cycle times, production volume, inspection sample size, measurement method, rejection rate and accuracy tolerance.
How to validate a comparable project: review part drawings, wood species, tooling, fixtures, machine configuration, cycle-time definition, sample size, inspection method and test date before comparing results.
Related Planning Resources

Use the project record to start a comparable evaluation

These resources help connect a real workpiece and process requirement to a practical equipment discussion.

Case FAQ

Questions buyers ask about this implementation

Does this case publish a verified throughput improvement?
No. Earlier public wording included a throughput figure, but the published project materials do not include the baseline, time-study method, part mix, sample size or test date needed to verify it. This case now reports the documented implementation rather than a universal production result.
Does this case publish a verified machining-accuracy tolerance?
No. The project record notes acceptance and test machining, but it does not publish a measurement report, inspection method, drawing tolerance or sampling plan. Accuracy for a new project should be agreed against its own drawing, material, fixture and measurement method.
What is documented for the Danwood workflow?
The public record identifies a 16-head machining center, a five-side machining center, chair and solid-wood component processing, delivery, installation, operator training and an ongoing technical-support workflow.
What should a factory provide for a comparable evaluation?
Provide part drawings, wood species, current process steps, required operations, batch size, target cycle time, quality requirements, factory layout and available utilities. Jasper can then define the appropriate test part and validation plan.